


Reloading Die Instructions
Prior to use, it is recommended to clean the die body using your standard bore cleaning method.
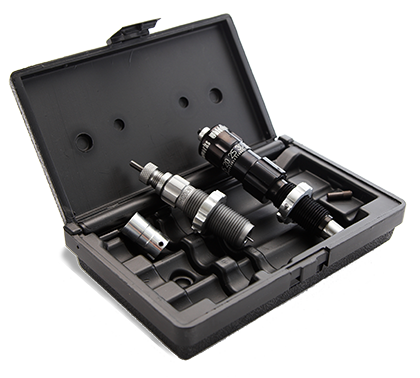
SEATER DIE INSTRUCTIONS
- Raise the ram on your press and screw the seater die into the press until it contacts the shellholder. Lower the ram and screw the die down 1-2 turns. Raise the ram and make sure the sleeve is moving 1/8” to 1/4” with the ram all the way up.
- Tighten the Lock Ring.
- When adjusting the seating depth, put the micrometer adjustment on 0. Then loosen the lock nut on the top of the micrometer, raise the threaded stem up 1”, and raise the ram up with the bullet and brass in place. Screw the threaded stem down until it touches the bullet (it will stop), lower the ram and then turn the threaded stem 1 to 2 turns down. Tighten the lock nut on the top of the micrometer and adjust the micrometer to obtain the desired seating depth.
SIZER DIE INSTRUCTIONS
- Check that the decap pin extends below die by about .150”. Adjust this by removing the decap assembly from the die, loosening the lock nut on the stem, and turning the stem. Tighten the lock nut and reinstall.
- Raise the ram on your press and screw the die in the press until it contacts the shell holder.
- Tighten the lock ring.
- Install the shoulder bump gauge onto the jaws of your calipers and tighten the set screw.
- Measure a piece of fired brass and record the length using the shoulder bump gauge.
- Lube and size the brass.
- Remeasure the sized brass to determine how far the shoulder of the case has been set back. We suggest about .002”–.003” for most bolt actions, and near .005” for other action types. It is also suggested to use an average measurement after sizing 3 pieces of brass. Due to variations in the brass, each piece will not be sized exactly the same.
- Adjust the amount of sizing by loosening the lock ring and turning the die in or out of your press. Each full turn of the die is .071”, so you won’t have to turn the die very far to make a noticeable adjustment.
